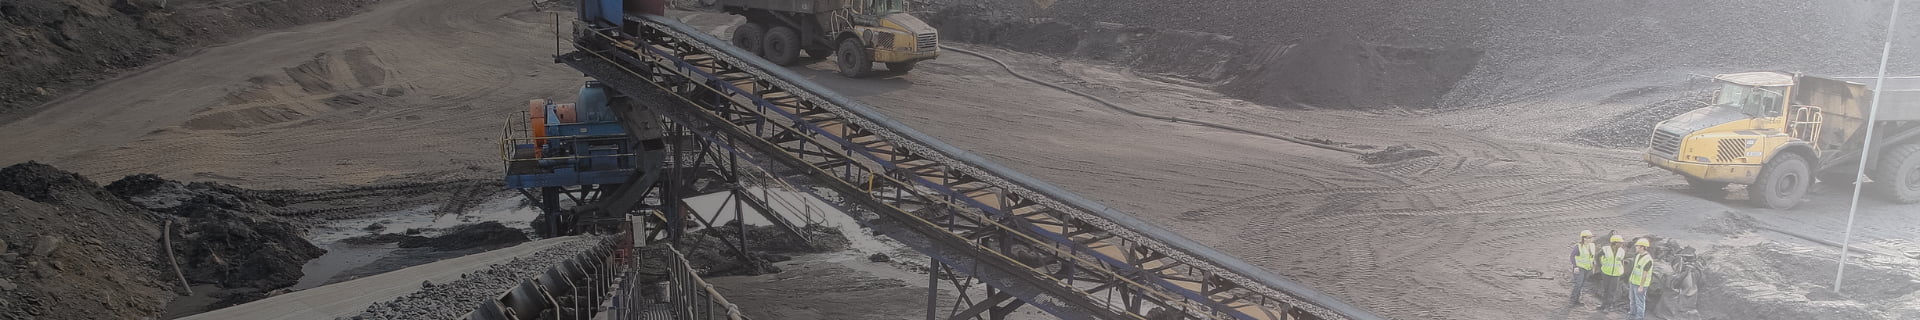
Have you ever wondered how millions of tons of raw materials and industrial products are transported efficiently through mines, cement plants, steel mills, power plants, ports, and heavy manufacturing facilities every day? From moving coal, ores, aggregates, and other bulk materials in mining operations to handling industrial materials throughout production and processing facilities, industrial conveyor belts have become one of the most essential material handling solutions worldwide. However, with different conveyor belt structures designed for various industrial environments, how can you choose the right belt for your application, operating conditions, and material transportation requirements? How can you improve conveying efficiency, reduce maintenance costs, and ensure long-term reliable operation?
This article is a complete guide to understanding the 8 most common types of industrial conveyor belts used in global industries. Whether you are a mining company, cement manufacturer, steel producer, power plant operator, quarry owner, or industrial equipment buyer, this guide will help you explore different types of industrial conveyor belts, understand their key features and applications, and select the most suitable conveyor belt solution for your heavy-duty material handling needs.
Comparison of 8 Types of Industrial Conveyor Belts
| Type | Material | Best For | Advantages | Industries |
|---|---|---|---|---|
| Rubber Conveyor Belt | Rubber, Fabric Reinforced Rubber, Steel Cord Rubber | Heavy-duty bulk material handling | High abrasion resistance, strong load capacity, excellent impact resistance, long service life | Mining, Quarrying, Cement, Steel, Coal, Power Plants |
| Steel Cord Conveyor Belt | Rubber with High-strength Steel Cords | Long-distance and ultra-heavy material transportation | High tensile strength, low elongation, excellent durability for large-scale projects | Large Mining, Coal Mines, Ports, Steel Plants |
| EP Conveyor Belt | Polyester and Nylon Fabric Reinforced Rubber | General industrial material conveying | Good strength, flexible structure, impact resistance, cost-effective performance | Cement Plants, Mining, Quarrying, Aggregate, Coal Handling |
| Nylon Conveyor Belt | Nylon Fabric Reinforced Rubber | Heavy-duty and impact-resistant conveying | Excellent flexibility, strong shock resistance, good fatigue resistance | Coal Mining, Underground Mining, Quarrying, Construction Materials |
| Heat Resistant Conveyor Belt | Heat Resistant Rubber Compound with Fabric or Steel Reinforcement | High-temperature material transportation | Resists high temperatures, maintains stable performance, durable under harsh conditions | Steel Plants, Cement Factories, Foundries, Metallurgy |
| Oil Resistant Conveyor Belt | Oil Resistant Rubber Compound with Fabric Reinforcement | Transportation of oily and grease-contaminated materials | Excellent oil resistance, prevents rubber swelling, extends service life | Chemical Plants, Steel Processing, Recycling, Metallurgy |
| Chevron Conveyor Belt | Rubber Conveyor Belt with Raised Surface Patterns | Inclined and steep-angle conveying | Improves grip, prevents material rollback, enhances conveying stability | Mining, Quarrying, Sand and Gravel Plants, Cement |
| Pipe Conveyor Belt | Flexible Rubber Belt with Reinforcement Layers | Enclosed and complex-route bulk material transportation | Reduces material spillage, protects conveyed materials, suitable for long-distance conveying | Mining, Power Plants, Ports, Chemical Industries |
How Many Types of Conveyor Belts Are There?
There are many different types of conveyor belts available for industrial applications, and each type is designed to solve specific transportation challenges. Based on material, structure, and working environment, the 7 most common types of industrial conveyor belts include rubber conveyor belts, PVC conveyor belts, PU conveyor belts, modular plastic conveyor belts, cleated conveyor belts, sidewall conveyor belts, and steel conveyor belts. Understanding their characteristics and applications is the key to choosing the right conveyor belt for your production needs.
1. Rubber Conveyor Belt
Rubber conveyor belts are one of the most widely used heavy duty conveyor belt types worldwide. Known for their excellent abrasion resistance, high tensile strength, and ability to handle heavy loads, rubber belts are the preferred solution for industries that transport large volumes of bulk materials over long distances. They are especially suitable for demanding environments where durability and impact resistance are critical.
Key Features:
- High wear resistance for continuous operation
- Strong load-bearing capacity for heavy materials
- Excellent impact resistance in harsh working conditions
- Suitable for long-distance bulk material conveying
Applications:
Mining, quarrying, cement plants, steel production, coal handling, power plants, ports, and bulk material transportation.
2. Steel Cord Conveyor Belt
Steel cord conveyor belts are designed for heavy duty and long-distance industrial conveying applications. Reinforced with high-strength steel cords inside the rubber structure, they provide superior tensile strength, low elongation, and excellent durability for transporting extremely heavy materials under demanding conditions.
Key Features:
- High tensile strength for heavy load transportation
- Low elongation for stable long-distance operation
- Excellent durability in harsh industrial environments
- Suitable for large-scale mining and bulk handling projects
Applications:
Large-scale mining, coal mines, ports, steel plants, and long-distance bulk material transportation.
3. EP Conveyor Belt
EP conveyor belts are widely used fabric reinforced conveyor belts made with polyester and nylon layers. They offer a good balance of strength, flexibility, impact resistance, and cost efficiency, making them one of the most common choices for general industrial material handling.
Key Features:
- High strength and good flexibility
- Excellent impact and abrasion resistance
- Stable performance under continuous operation
- Cost-effective solution for general industrial conveying
Applications:
Cement plants, mining, quarrying, coal handling, aggregate production, and industrial bulk material transportation.
4. Nylon Conveyor Belt
Nylon conveyor belts use nylon fabric as the reinforcement layer, providing excellent flexibility, shock resistance, and fatigue resistance. They are suitable for industrial applications where frequent bending, impact loads, and complex operating conditions are required.
Key Features:
- Excellent flexibility for demanding conveying conditions
- Strong impact resistance for heavy materials
- Good fatigue resistance during continuous operation
- Suitable for underground and heavy industrial applications
Applications:
Coal mining, underground mining, quarrying, construction materials, and heavy material handling.
5. Heat Resistant Conveyor Belt
Heat resistant conveyor belts are specially designed for transporting high-temperature materials in industrial environments. Made with heat-resistant rubber compounds, they maintain reliable performance when handling hot materials that may damage standard conveyor belts.
Key Features:
- Excellent resistance to high-temperature materials
- Stable performance under continuous heat exposure
- Improved durability in harsh industrial conditions
- Designed for high-temperature bulk material conveying
Applications:
Steel plants, cement factories, foundries, metallurgy industries, and high-temperature material transportation.
6. Oil Resistant Conveyor Belt
Oil resistant conveyor belts are manufactured with special rubber compounds that provide resistance against oil, grease, and oily materials. They are suitable for industrial environments where standard rubber belts may suffer from swelling, damage, or reduced service life.
Key Features:
- Excellent resistance to oil and grease contamination
- Reduced rubber swelling and material degradation
- Reliable performance in industrial processing environments
- Longer service life when handling oily materials
Applications:
Chemical plants, metallurgy, industrial recycling, steel processing, and oily material transportation.
7. Chevron Conveyor Belt
Chevron conveyor belts feature raised patterns on the belt surface to improve grip and prevent material rollback during inclined conveying. They are widely used in industrial applications where bulk materials need to be transported at higher angles.
Key Features:
- Enhanced grip for inclined conveying
- Prevents material sliding during transportation
- Suitable for heavy bulk material handling
- Improves conveying efficiency on steep slopes
Applications:
Mining, quarrying, sand and gravel plants, cement production, and inclined bulk material transportation.
8. Pipe Conveyor Belt
Pipe conveyor belts are specially designed to form a closed tubular shape during operation, allowing materials to be transported with reduced spillage and environmental impact. They are suitable for complex routes and applications requiring enclosed bulk material conveying.
Key Features:
- Enclosed transportation to reduce material spillage
- Protects conveyed materials from external conditions
- Suitable for complex conveying routes
- Provides cleaner operation for industrial environments
Applications:
Mining, power plants, ports, chemical industries, and long-distance enclosed bulk material transportation.
Frequently Asked Questions
1. Which conveyor belt should I use for high-temperature materials in steel and cement plants?
Standard rubber conveyor belts may quickly deteriorate when continuously exposed to hot materials such as cement clinker, sinter, or foundry materials. For these applications, use heat resistant conveyor belts designed for elevated temperature conditions. The correct belt grade depends on actual material temperature, but industrial buyers should evaluate continuous operating temperature rather than short-term peak temperature to avoid premature cracking, hardening, and cover separation.
2. How can I stop my conveyor belt from tearing when transporting heavy materials?
Conveyor belt tearing commonly happens when sharp materials, oversized rocks, or metal fragments impact the belt surface. For mining, quarrying, and aggregate industries, select belts with higher tear resistance, such as steel cord conveyor belts or reinforced rubber conveyor belts with strong fabric layers. In addition, installing proper impact protection at loading points and controlling the maximum feed size of materials can reduce sudden belt damage and prevent unexpected production shutdowns.
3. Why does my conveyor belt run to one side during operation?
Belt mistracking is one of the most common industrial conveyor problems and is usually caused by misaligned pulleys, uneven material loading, worn rollers, or incorrect belt tension. Before replacing the belt, check whether the conveyor frame is level, whether rollers are aligned within the same centerline, and whether materials are distributed evenly across the belt width. In many cases, correcting alignment and tension problems can solve tracking issues without replacing the entire conveyor belt.
4. What conveyor belt is suitable for transporting abrasive materials like stone, coal, and ores?
For abrasive industrial materials such as crushed stone, coal, iron ore, and minerals, rubber conveyor belts are usually the most suitable option because they provide better wear resistance and impact protection than lighter belt materials. For extremely abrasive applications, select belts with thicker rubber covers and higher abrasion resistance ratings. Steel cord conveyor belts are recommended for large mining operations where both abrasion resistance and long-distance transportation strength are required.
5. How do I choose between EP conveyor belts and steel cord conveyor belts?
The choice between EP conveyor belts and steel cord conveyor belts mainly depends on transportation distance, load capacity, and operating conditions. EP conveyor belts are commonly used for medium-distance industrial conveying because they provide good strength, flexibility, and cost efficiency. Steel cord conveyor belts are better for large mining and bulk material projects where conveying distances exceed several kilometers or where extremely heavy loads require higher tensile strength and lower belt elongation.
Conclusion
Understanding the different types of industrial conveyor belts is the first step toward improving material handling efficiency in heavy-duty industries. From rubber conveyor belts and EP conveyor belts for mining, cement, and bulk material handling to steel cord conveyor belts for long-distance transportation and heat resistant conveyor belts for high-temperature environments, each industrial conveyor belt type is designed for specific operating conditions. For mining companies, cement manufacturers, steel plants, power plants, quarry operators, and industrial equipment buyers, selecting the right conveyor belt based on material characteristics, load capacity, transportation distance, and working environment can help reduce unexpected downtime, lower maintenance costs, and improve long-term production efficiency.
As an experienced industrial conveyor belt manufacturer, JH Conveyor Belts provides customized conveyor belt solutions for mining, bulk material handling, cement production, steel manufacturing, power plants, and other industrial applications. Whether you need a heavy duty rubber conveyor belt, abrasion-resistant conveyor belt, steel cord conveyor belt, or a customized industrial conveyor belt solution, our team can help you select the right belt according to your operating conditions and material handling requirements. Visit us to learn more about our industrial conveyor belt products and contact us for professional support and customized solutions.